EN


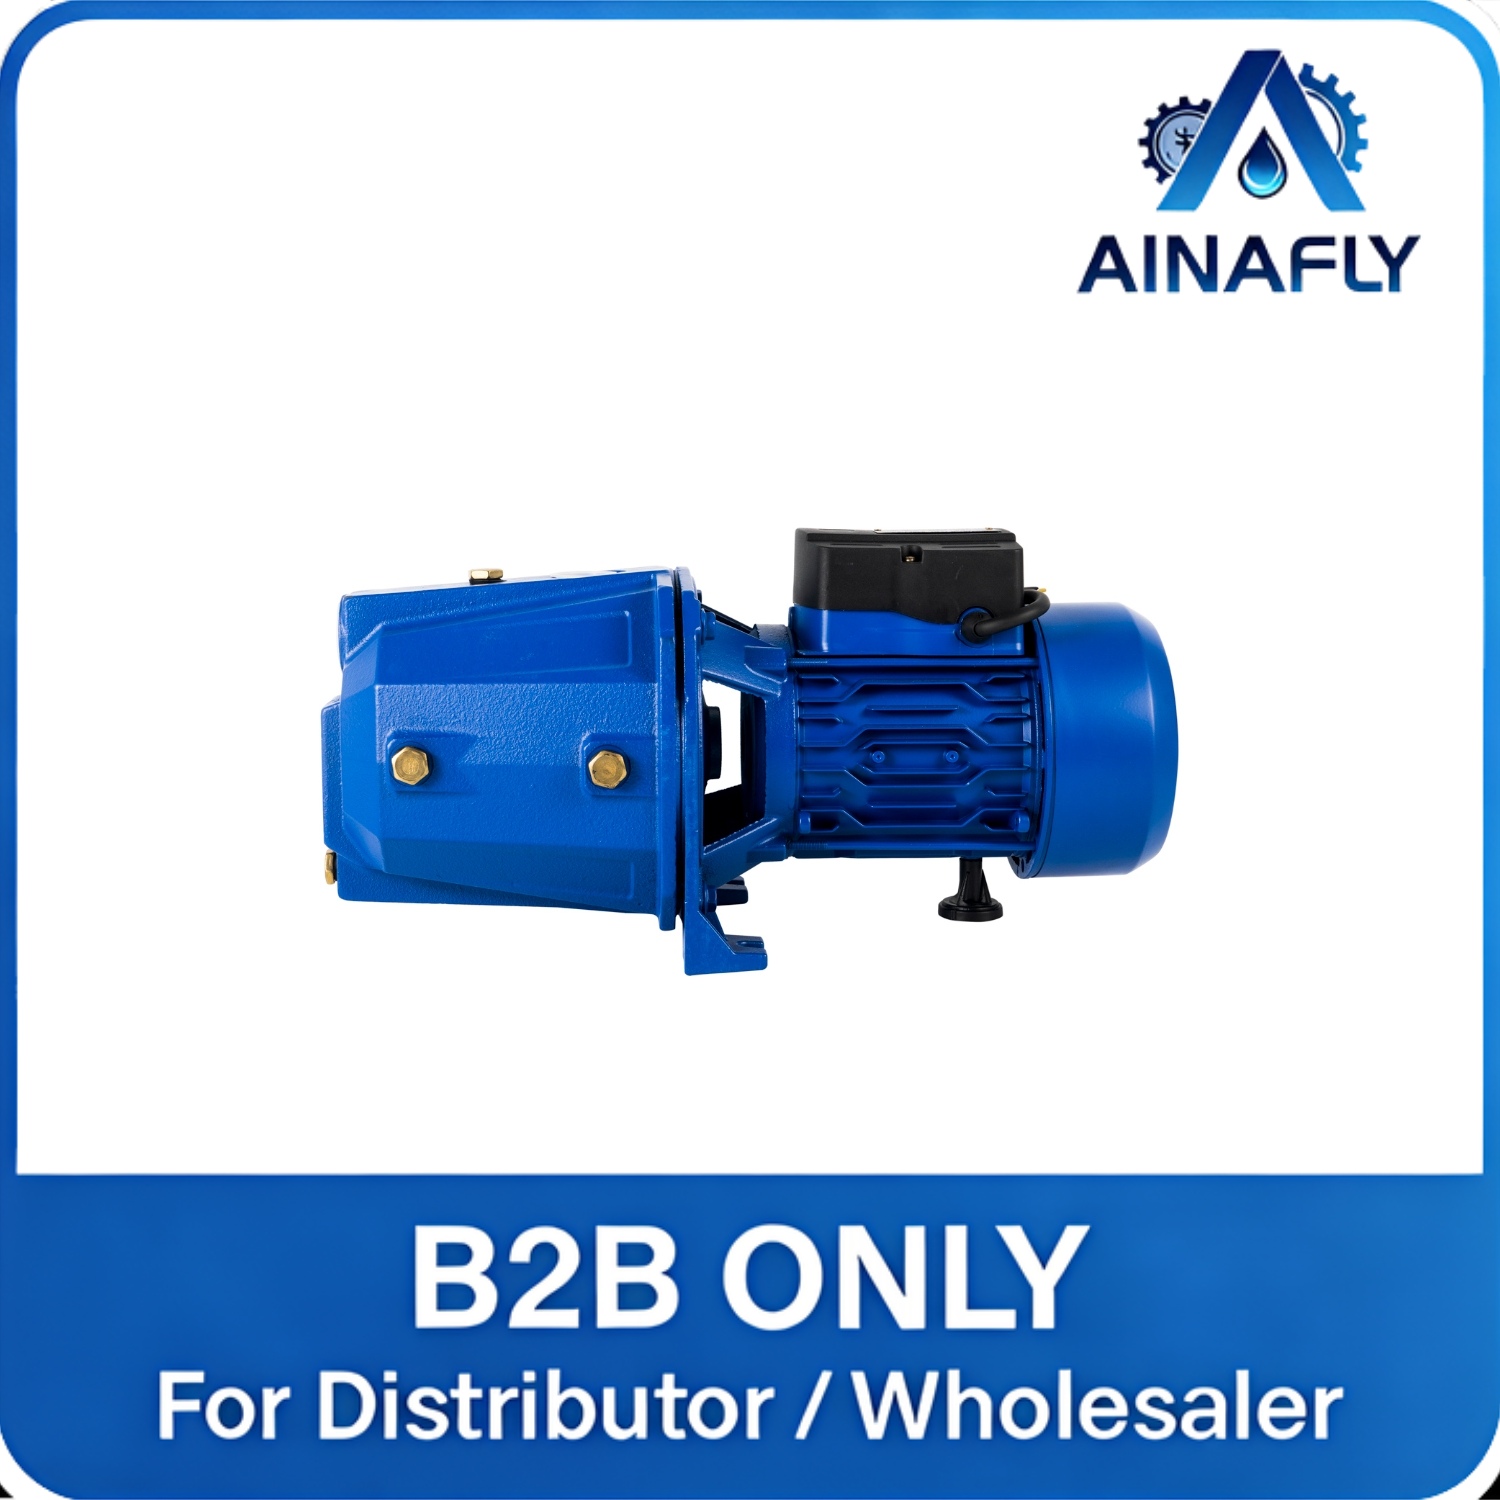
AINAFLY HFM Series Heavy Duty Centrifugal Water Pump for Irrigation and Water Transfer
-
Heavy-Duty Performance
Cast iron construction for stable and reliable operation. -
Self-Priming Design
Up to 7–8m suction depth for easier water transfer. -
High Efficiency
Centrifugal design delivers steady flow with lower energy consumption. -
Wide Voltage Support
Available for 220V and 380V power systems. -
Wide Applications
Ideal for irrigation, construction, household water supply and industrial use.

- Overview
- Recommended Products
Description:
Product General Information:
Place of Origin: |
Zhejiang Taizhou |
Brand Name: |
AINAFLY Pump |
Commercial Terms of Products:
Minimum Order Quantity: |
100PCS |
Packaging Details: |
CARTON |
Delivery Time: |
20~35DAYS |
Payment Terms: |
T/T |
✅ Product Advantages – Why Choose AINAFly HFM Land Pump?
1. Heavy-Duty Cast Iron & Robust Motor for Long-Lasting Performance
Built with high-strength cast iron casing and a powerful industrial motor, this pump delivers stable, high-efficiency water transfer even under continuous or heavy-load operation. Designed to withstand harsh environments — perfect for Africa, Middle East, and Southeast Asia’s demanding climates and working conditions.
2. Self-Priming & High Efficiency for Easy Operation
Equipped with a self-priming mechanism, it can automatically draw water from a depth of up to 7–8 meters without manual priming — saving time and labor. The centrifugal design ensures smooth, consistent flow with low energy consumption, reducing operational costs.
3. Wide Voltage Compatibility – 220V / 380V Support
Flexible voltage support (220V single-phase or 380V three-phase) makes it ideal for both household and industrial use — whether you’re running it from a generator in rural areas or connecting to grid power at construction sites or factories.
4. Anti-Corrosion & Weather-Resistant Design
The pump’s surface is treated with anti-rust coating, and internal components are corrosion-resistant — ensuring reliable performance in humid, dusty, or saline environments common in tropical and coastal regions.
5. Easy Installation & Low Maintenance
With a compact, integrated design and standard flange connections, it’s quick to install and easy to maintain. Minimal moving parts reduce breakdown risks — keeping your operations running smoothly with less downtime.
🌍 Application Scenarios – Where AINAFly HFM Pump Shines
1. Agricultural Irrigation Systems
Perfect for small to medium farms in arid or semi-arid regions — efficiently pump water from wells, rivers, or reservoirs to fields. Ideal for crops like rice, maize, sugarcane, and vegetables.
2. Construction Site Water Supply
Used to transfer water for concrete mixing, dust suppression, equipment washing, and worker hydration — a must-have for infrastructure projects across Africa, Southeast Asia, and the Middle East.
3. Residential & Community Water Supply
Ideal for pumping water into overhead tanks, homes, or villages where municipal water pressure is low or unavailable. Great for rural electrified communities or off-grid solar-powered setups.
4. Industrial & Commercial Use
Suitable for factories, food processing plants, laundry services, and car washes — delivering high-volume water flow with stable prure foress cleaning, cooling, or production needs.
5. Emergency & Disaster Relief
Reliable in remote or disaster-affected areas where infrastructure is damaged — easily powered by generator or solar inverter, making it a critical tool for humanitarian water supply operations.
Specifications:


(Different configurations available according to market requirements.)
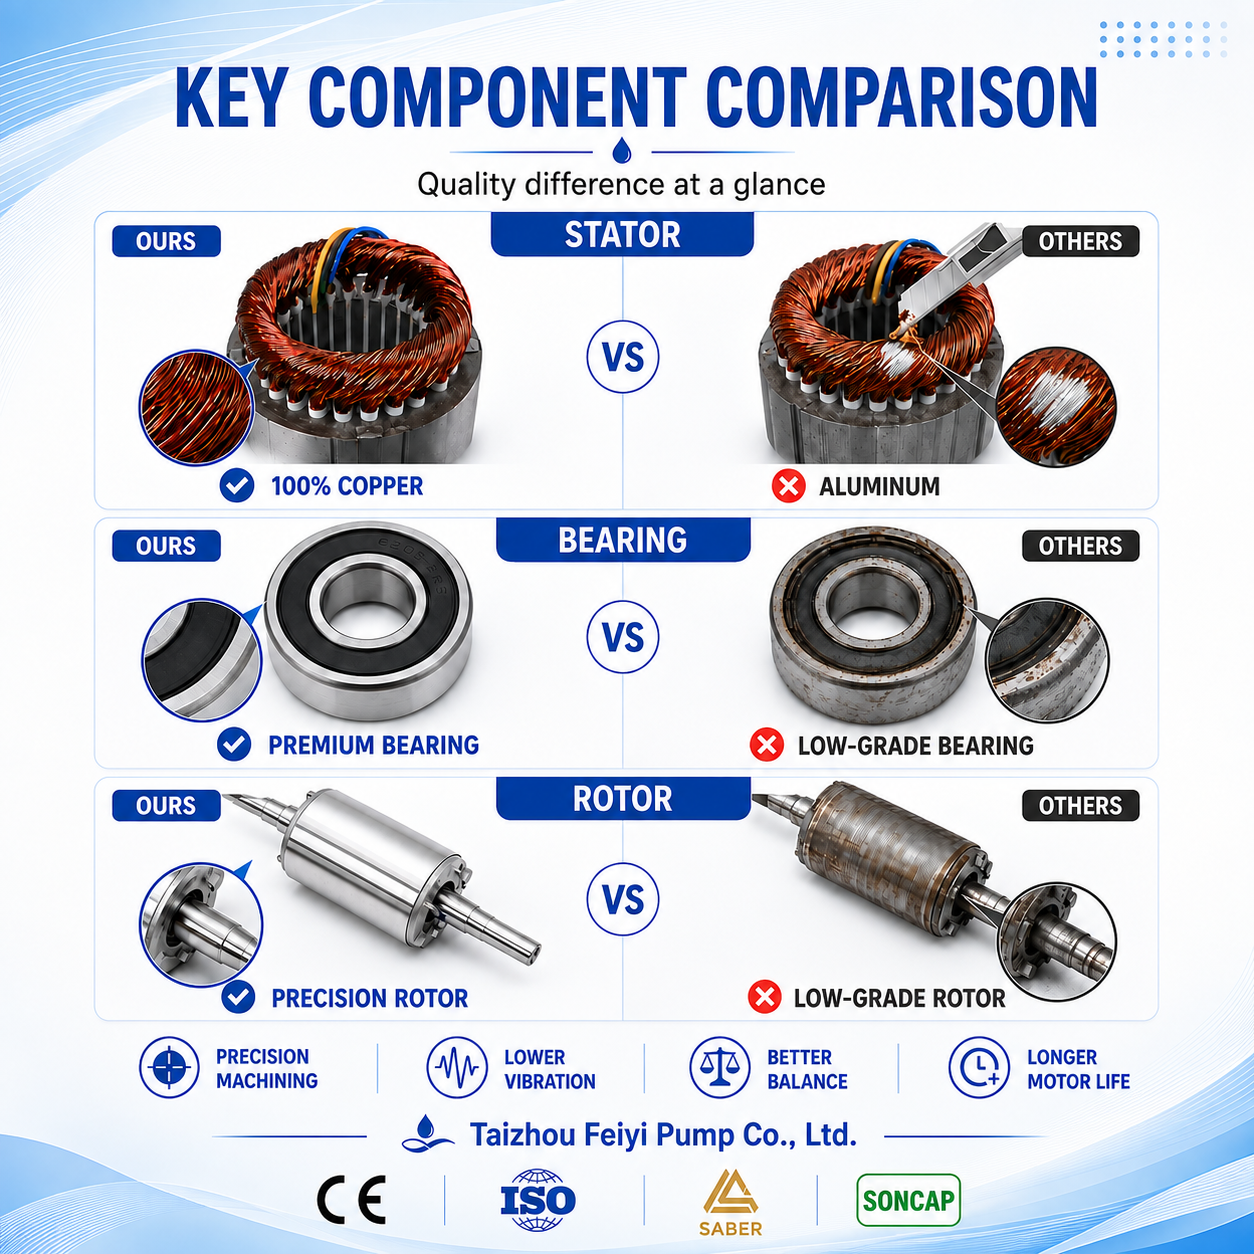
Premium Core Components for Stable and Long-Term Performance
Our pumps are built with carefully selected core motor components, including a 100% copper-wire stator, premium-quality bearings, and a precision-machined rotor. These components work together to provide stable conductivity, smooth rotation, better dynamic balance, and reliable motor performance during continuous operation.
Compared with aluminum windings, low-grade bearings, and poorly machined rotors, our upgraded component design helps reduce vibration, minimize mechanical wear, improve operating stability, and extend overall motor service life. By focusing on the quality of every critical internal part, we ensure more consistent performance and greater long-term reliability.
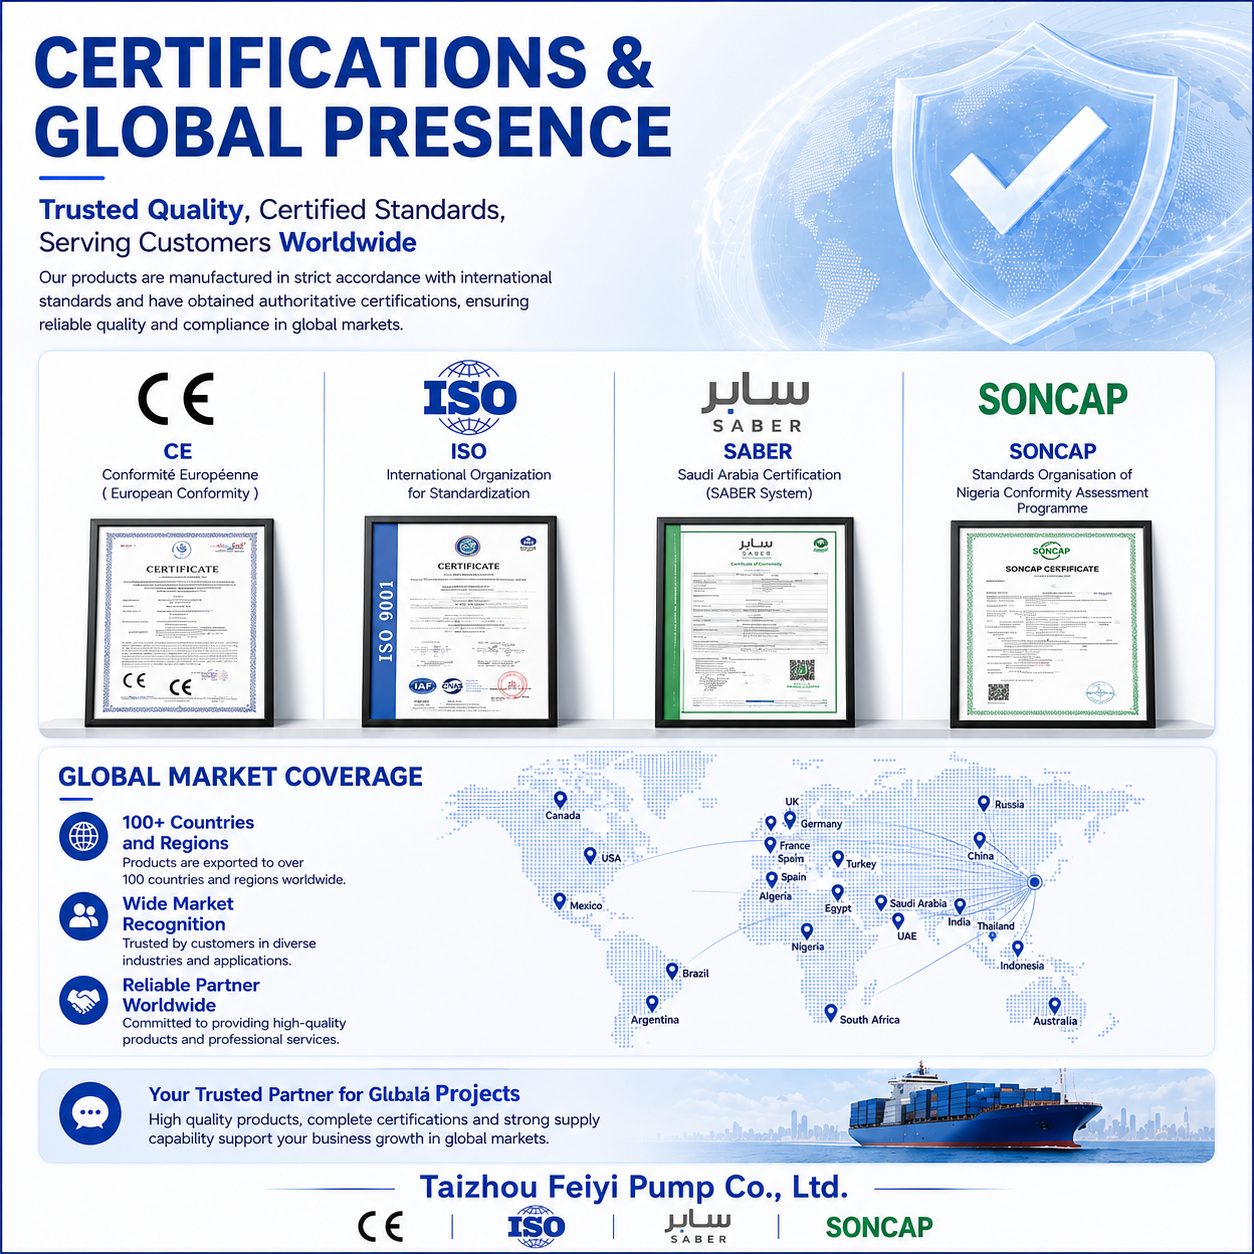
Certified Quality and Global Market Presence
Taizhou Feiyi Pump Co., Ltd. manufactures products in accordance with international quality and compliance standards and has obtained recognized certifications including CE, ISO, SABER, and SONCAP. These certifications help ensure that our products meet the technical, safety, and market access requirements of different countries and regions.
With products supplied to more than 100 countries and regions worldwide, we serve customers across Europe, the Middle East, Africa, Southeast Asia, North and South America, and other global markets. Supported by reliable product quality, complete certification solutions, and professional export services, we are committed to becoming a trusted long-term partner for distributors, importers, OEM brands, and international projects.
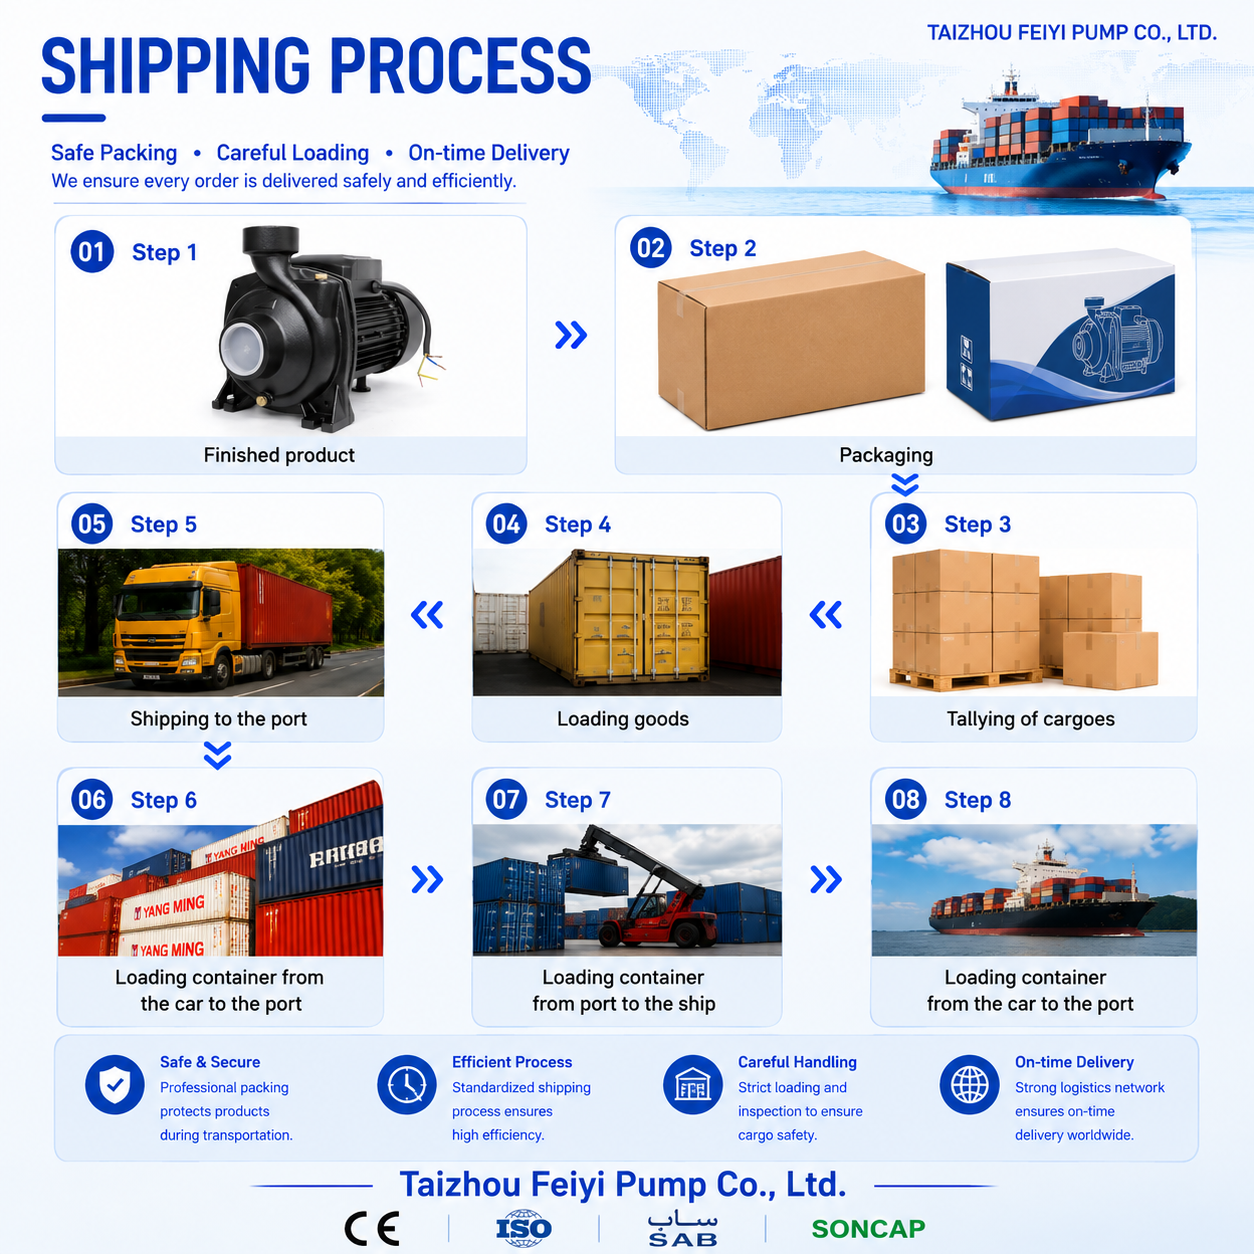
Standardized Shipping Process for Safe and On-Time Delivery
Taizhou Feiyi Pump Co., Ltd. follows a complete and standardized shipping process to ensure every order is packed, handled, and delivered safely and efficiently. From finished product preparation and secure packaging to cargo tallying, container loading, port transportation, and final vessel shipment, each step is carefully managed by our team.
Our professional packing helps protect products during transportation, while strict cargo counting and loading inspections reduce the risk of missing or damaged goods. With coordinated logistics support and a reliable shipping network, we are committed to providing safe handling, efficient processing, careful loading, and on-time delivery for customers worldwide.